Home
News
About Us
Contact Us
Yuepu Innovation Center R&D · Membrane · Equipment Group Headquarters Operations & Global Services Membrane R&D Center Details › Equipment Workshop Details › Spiral-Wound Membrane Details › Hollow-Fiber Membrane Details › Ceramic Membrane Details ›
ABOUT BONA TECH

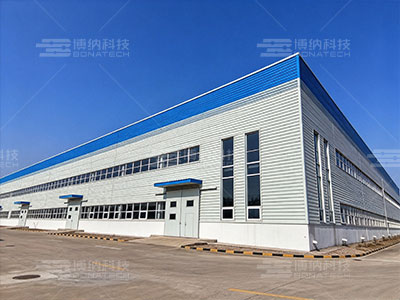
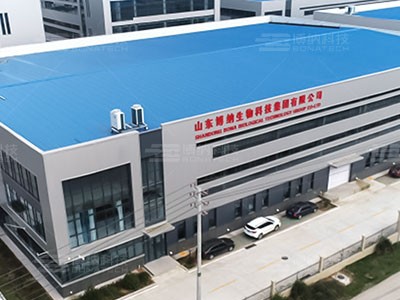
Manufacturing Base

Integrated membrane separation solutions — from R&D and manufacturing to service.

Who We Are

Membrane Separation & Purification Specialists

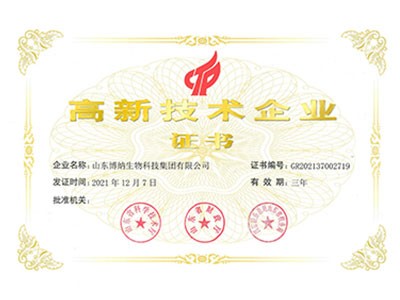
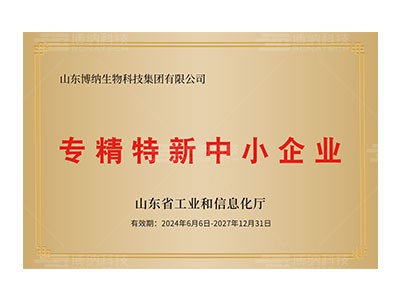
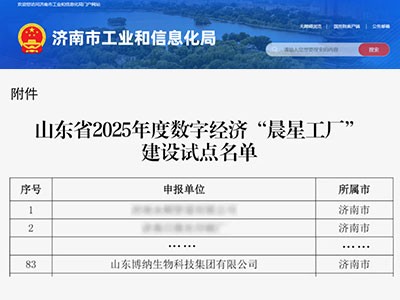
Founded in 2012, Shandong Bona Biotechnology Group Co., Ltd. is a high-tech enterprise specializing in material extraction, separation, and purification. In 2019, the company consolidated its business units and adopted a group operating structure. It is recognized as a National High-Tech Enterprise and holds EU CE marking together with ISO 9001 (Quality), ISO 14001 (Environment), and ISO 45001 (Occupational Health & Safety) certifications, among other domestic and international standards. The group has also been named a provincial "Specialized, Sophisticated, Differentiated & Innovative" enterprise, a provincial innovative SME, a municipal Gazelle enterprise, and a "Morning Star Factory" pilot enterprise.

Today, BonaTech is a leading Chinese supplier of membrane materials and application systems, delivering integrated separation and purification solutions to customers worldwide. Our technology serves industry and is equally trusted by the academic community: more than 1,000 research institutions worldwide use BonaTech membrane separation equipment, and our systems have been featured in nearly 400 published papers. This track record reflects both the proven performance of our equipment and the scientific rigor of the researchers who rely on it.

High-Tech Enterprise ISO 9001 Quality System CE / GMP Compliance In-House Membrane Element Lines Custom (Non-Standard) Engineering Full-Cycle Service
High-Tech Enterprise
ISO 9001 Quality Management
CE (EU Safety Compliance)
GMP (Good Manufacturing Practice)
By The Numbers

BonaTech at a Glance

Fourteen years in membrane separation — measured by the customers, capacity, and markets we serve.

14
Years

Deep Expertise in Membrane Separation

4,000
+
Customers

Served Worldwide

1,500
Units

Annual Capacity

10,000
m²

Production Floor Area

50
+
Countries & Regions

Served Worldwide

Milestones

Our History

From one laboratory to a modern manufacturing campus — a decade of growth driven by customer separation challenges.

2012

Company Founded, Focused on Membrane Separation R&D

BonaTech was founded with a core R&D team established, setting the direction of serving separation and purification processes with membrane separation technology.

Company Founded, Focused on Membrane Separation R&D
2014

Long-Term Strategic Partnerships

Built long-term, stable strategic partnerships with numerous universities and pharmaceutical companies (e.g., Jiangzhong Group, Qilu Pharmaceutical).

Long-Term Strategic Partnerships
2016

Technical Service Center Established

Established a technical service center to provide repair and maintenance for domestic and overseas laboratory instruments, delivering professional support to new and existing customers.

Technical Service Center Established
2017

Two Subsidiaries Established

Two subsidiaries were established; product coverage spans laboratory equipment, scientific instruments, membrane elements, and membrane filtration systems in R&D and manufacturing.

Two Subsidiaries Established
2018

Acquired Two Membrane Manufacturers

Acquired two membrane manufacturers, extending the business scope upstream and downstream while maintaining the overall product portfolio.

Acquired Two Membrane Manufacturers
2019

Group Structure Formed

Transitioned to group-based management in response to market demand and strategic growth, and was renamed Shandong Bona Biotechnology Group Co., Ltd.

Group Structure Formed
2021

High-Tech Enterprise Certified

Realigned the industrial structure and upgraded products, accelerating the path of technology-driven innovation.

High-Tech Enterprise Certified
2023

Group Output Doubled

Group output doubled; continued to strengthen IP portfolio development and technical standards, further expanding its scale.

Group Output Doubled
2024

Series A Funding Completed

Completed Series A financing, raising a total of nearly RMB 100 million.

Series A Funding Completed
2024

Shandong SRDI Enterprise

Recognized as a 2024 Shandong Specialized, Sophisticated, Differentiated and Innovative (SRDI) enterprise for its innovative achievements in membrane separation and purification.

Shandong SRDI Enterprise
2024

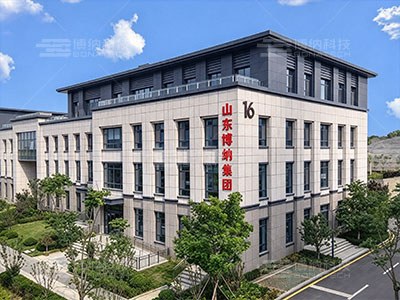
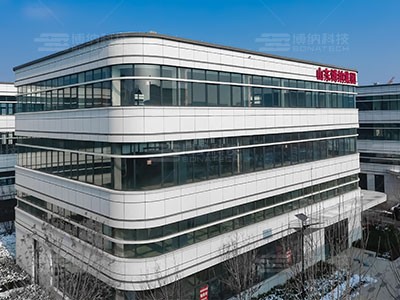
Yuepu Innovation Center HQ Opened

The headquarters building at the Yuepu Innovation Center officially opened, with R&D design centers and production bases in Jinan, Zibo, and other locations.

Yuepu Innovation Center HQ Opened
2025

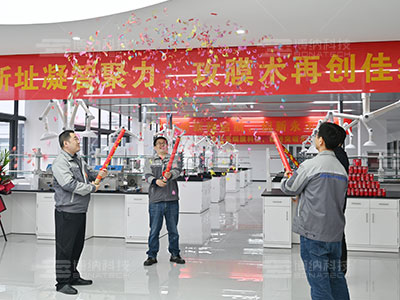
R&D Center Relocated

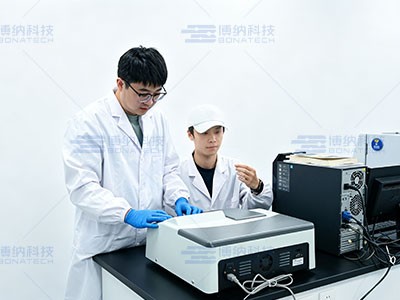
Relocated the R&D center to a new 2,000 m2 laboratory at the Yuepu Center, integrating an independent innovation R&D zone, application lab, pilot-scale platform, and customer experience center.

R&D Center Relocated
2025

Shandong 2025 Morning Star Factory Pilot Enterprise

Selected as a 2025 Shandong Morning Star Factory pilot enterprise for its outstanding performance in digital smart manufacturing, becoming a benchmark for manufacturing digital transformation in Shandong.

Shandong 2025 Morning Star Factory Pilot Enterprise
Our Advantages

Why Choose BonaTech

From proprietary membrane technology to compliant, turnkey delivery — the reasons global buyers trust BonaTech for separation and purification

Full Product Range

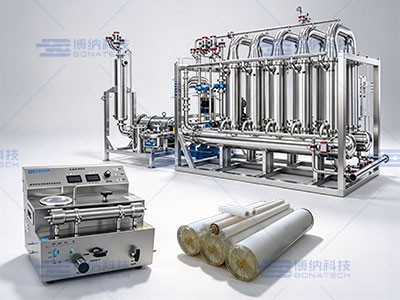
A full portfolio across TFF, ultrapure water, and exosome systems — in dozens of models spanning lab, pilot, and industrial scales.

Proprietary Core Technology

We control the full chain — membrane chemistry, element fabrication, and system integration — keeping core components in-house for consistent quality and supply security.

Industry Process Know-How

Years of process data and field cases across biopharma, food, and chemicals yield proven routes for concentration, purification, desalination, and clarification.

Internationally Compliant Quality

Certified to ISO 9001, CE, and GMP, with materials meeting FDA, USP Class VI, and 3-A — compliance that clears export and audit hurdles.

Custom & Turnkey Solutions

From process design and manufacturing to on-site installation and commissioning, we deliver tailored, turnkey systems built around your process — not off-the-shelf compromises.

Full-Cycle Service

Dedicated application engineers support you end-to-end — from selection and installation training to consumables and responsive after-sales — across the full equipment lifecycle.

Compliance

Compliance & Certifications

Certifications and documentation built for regulated industries — so your equipment clears validation, audits, and export with confidence.

GMP GMP Compliance Biopharma · Food & Beverage
FDA FDA-Compliant Biopharma
CE CE Certified All Industries (EU Export)
ISO ISO 9001 All Industries
USP USP Class VI Biopharma
3A 3-A Sanitary Standards Food & Beverage

Not sure which system fits your process?

Tell us about your process — our application engineers will get back to you within one business day with a recommended configuration and a tailored quote.

Request a Quote